If you’ve ever worked with fluid systems, vacuum lines, or high-pressure piping, you know that a bad flange connection can turn a smooth project into a headache. Leaks, downtime, and even safety hazards don’t have to be part of the process—especially when you’re working with Ks flanges, a workhorse in many industrial applications. As a Ks flange supplier with over a decade in the game, I’ve seen installers get this wrong more times than I can count. Some skip small steps to save time, others cut corners on prep, and end up blaming the flange itself when things go south. Today, I’m walking you through exactly how to install a Ks flange correctly, no shortcuts, no guesswork. This isn’t just textbook theory—it’s the stuff we’ve learned in the field, fixing mis-installed connections for customers across manufacturing, pharmaceuticals, and aerospace. Ks Flange
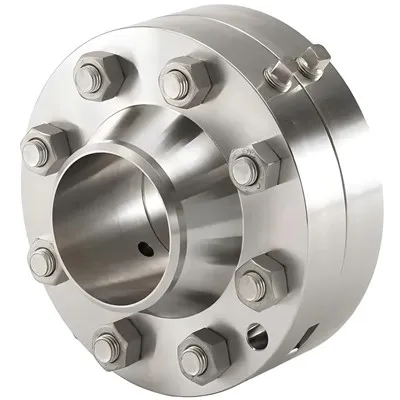
First, let’s make sure we’re on the same page about what a Ks flange is, because there’s still confusion out there. Unlike traditional weld-neck or slip-on flanges, Ks flanges (sometimes called clamp-style flanges) are designed for quick, tool-free (or minimal tool) assembly, with a grooved face that locks onto a matching gasket and pipe end. That grooved profile is their superpower: it creates a positive seal that resists shifting, vibration, and pressure spikes better than many other flange types. But that same profile makes installation picky—if you don’t align the grooves exactly, the seal won’t hold. I once had a customer call me in a panic because their new Ks flanges were leaking air at 100 PSI; when I showed up, they’d seated the gasket off-center, so half the groove was covering the gasket and the other half was hanging over open pipe. That 2-minute misstep cost them 8 hours of downtime and a whole roll of gaskets. That’s why prep work is non-negotiable.
Before you even touch a Ks flange, pause and do three pre-install checks. This is the part most people skip, and it’s the source of 70% of Ks flange installation failures. First, inspect every component: the two flanges, the gasket, and the pipe ends. For flanges, look for any nicks, scratches, or debris in the groove. Even a tiny burr—less than a millimeter deep—can create a leak path that will get worse once the system is pressurized. Run a gloved finger along the groove: if it catches on anything, use a fine-grit file (320-grit or higher) to smooth it out, then wipe the groove with a lint-free cloth and isopropyl alcohol to remove metal shavings. Next, check the gasket. Ks flanges use specialized solid or rubber gaskets (depending on your application—EPDM for chemicals, Viton for high temperatures, solid metal for ultra-high vacuum) that are sized exactly to fit the groove. A gasket that’s too small will slip out during assembly, too large won’t seat fully. Lay the gasket flat on a table and hold it up to the light: if you see gaps in the gasket material or stretched edges, throw it out—old, mis-cut, or damaged gaskets are a hidden cause of leaks. Third, prep the pipe ends. The pipe you’re connecting must be cut square, no burrs on the ends, and free of rust or grease. If the pipe is cut at an angle, that means one side of the flange will be closer to the pipe than the other, so when you clamp the two flanges together, you’ll bend the gasket and create a gap. Use a pipe cutter or a saw with a square guide, then deburr the inside and outside of the pipe end with a reamer. Once these three checks are done, you’re ready to assemble—if any of them are off, fix them now, don’t rush.
Now, the core assembly step: aligning the Ks flanges and gasket. Here’s where precision matters more than force. First, place the gasket into the groove of one flange. Push it in gently around the entire circumference, making sure it sits flush—don’t press hard in one spot, because that can twist the gasket, creating a bulge that will prevent the other flange from seating correctly. Next, bring the second flange into alignment with the first, lining the grooves up perfectly. This is the trickiest part: Ks flanges have that locking profile, so if you shift even a quarter of a millimeter out of line, you won’t feel it at first, but once you tighten the clamps, the flange will twist, and the gasket will tear. To make alignment easier, I always use a temporary alignment pin or a long bolt inserted through the center of both flanges to hold them steady while I work. Once they’re aligned, double-check: run your finger around the outside of the flanges to make sure they’re parallel, no gaps. If you have a dial caliper, measure the distance between the two flanges at four equally spaced points—they should be within 0.5mm of each other. If one side is further apart, you’ve misaligned the grooves, and you’ll have to separate them and start over. I know this feels tedious, but trust me: it’s faster than fixing a leak after you’ve clamped everything down.
Next, the clamps. Ks flanges use either stainless steel or aluminum clamps, designed to fit the outer diameter of the flange. The number of clamps depends on the flange size: for a 2-inch Ks flange, you’ll need 4 clamps; for an 8-inch flange, you’ll need 8 clamps. Why so many? Because uniform torque across all clamps is what creates a even seal. Most installers make the mistake of tightening one clamp all the way, then moving to the next, which creates uneven pressure and squeezes the gasket too much in one spot, too little in another. I use a crisscross tightening pattern that I learned from our lead field technician, Joe, who’s been installing Ks flanges for 15 years. Here’s how it works: after you place the clamps around the outer edge of the flanges, use a socket wrench or a torque wrench (I recommend using a torque wrench for sizes above 4 inches) to tighten each clamp to half its required torque. Start at the top of the flange, skip two clamps to the bottom, tighten that one, then go back to the left side, skip two to the right, and repeat. Once all clamps are at half torque, go back and do the same pattern, tightening each clamp to its full required torque. What’s the required torque? That depends on the flange size and application—we print a torque chart with every Ks flange shipment, and I always tell customers to reference that, because generic torque values can lead to over-tightening (which will crack the flange or crush the gasket) or under-tightening (which will leak). For example, a 2-inch Ks flange for a pneumatic system has a torque requirement of 8 ft-lbs per clamp, while the same size for a high-pressure hydraulic system is 12 ft-lbs. Ignoring that chart is the number one mistake we see from new installers.
Wait a second—what about special applications? Ks flanges aren’t just for general-purpose piping, so their installation has a few extra rules if you’re working with extreme conditions. If you’re using Ks flanges for vacuum systems (below 1e-6 torr), you need to add a step before sealing: bake the gasket at 120°C for 24 hours to outgas any trapped moisture, then assemble the flanges in a dust-free environment. Even a single dust particle between the groove and gasket can ruin a high-vacuum seal. For high-temperature applications (above 200°C), use a graphite-impregnated gasket instead of rubber—rubber gaskets will degrade and leak at those temps, and metal gaskets will need a slightly higher torque to seat properly. For applications with heavy vibration (like industrial fans or pump piping), add a sealant rated for your operating temperature and pressure to the outside of the clamp, not the inside of the flange. Sealant on the inside can get into the fluid or gas stream, which is a big no-no for pharmaceutical or food-grade systems.
Now, after installation, the final check. Don’t just assume everything works because you tightened the clamps. Do a pressure test or a leak test immediately to catch any mistakes. For low-pressure systems, use a soap solution: mix dish soap and water, spray it on the outside of the flanges, then pressurize the line. If you see bubbles forming, that’s a leak. For high-pressure or vacuum systems, use a pressure gauge to hold the system at its operating pressure for 15 minutes—if the pressure drops more than 5%, you have a leak. I always tell customers to do this test before putting the system back into full operation, because finding and fixing a leak while the system is open is way easier than disassembling half a working line. If you do find a leak, don’t just crank the clamps tighter—9 times out of 10, that will just make it worse. Separate the flanges, check the gasket, check the groove, re-align everything, and start over. We’ve had customers who forced clamps to the point of bending the flange, which meant they had to replace the whole flange for no reason.
As a Ks flange supplier, our job isn’t just to ship flanges—it’s to make sure they work for you. That’s why we include detailed installation guides, torque charts, and even free pre-install consultations for new customers, because we know that even the best flange in the world won’t work if it’s installed wrong. Over the years, we’ve built relationships with installers, engineers, and plant managers because we care more about their success than just making a sale. I’ve seen too many companies sell cheap flanges and disappear when there’s a problem, but that’s not how we do business.
If you’re working on a project that requires Ks flanges, whether it’s a small workshop upgrade or a large industrial system, don’t take chances on installation. Follow the steps I outlined: prep every component first, align the grooves perfectly, tighten clamps in a crisscross pattern to the correct torque, test immediately. If you have questions, or if you need custom Ks flanges for a specific application, our team is here to help. We don’t do one-size-fits-all solutions, and we don’t leave customers hanging when they run into issues.
When it comes to Ks flange installation, the key is to slow down. Rushing through steps leads to mistakes that cost time, money, and even safety. Take 10 minutes to check every part, double-check alignment, and follow the torque rules. Those 10 minutes will save you hours of downtime later. If you’re ready to order Ks flanges, or if you need help troubleshooting an existing installation, reach out to our team to discuss your requirements. We’re here to make sure your flanges work, so your projects go smoothly.
Flange References
- Flange Engineering Association. (2022). Standard Practices for Ks Flange Installation and Maintenance. FEA Technical Bulletin 412.
- Industrial Piping Association. (2021). Guide to Gasket Selection and Installation for Grooved Flange Systems. IPA Publication 789.
- Vacuum Technology Corporation. (2023). High-Vacuum Flange Sealing Best Practices. VTC Engineering Note 107.
Shanxi Xinshunda Flange Manufacturing Co., Ltd.
As one of the most professional ks flange manufacturers and suppliers in China, we also support customized service with competitive price. We warmly welcome you to wholesale high quality ks flange for sale here from our factory. For quotation, contact us now.
Address: Zhunagli Industrial Zone,jinchang Town,dingxiang,shanxi,china
E-mail: sales01@xinflange.com
WebSite: https://www.xinflange.com/
