Hey there! I’m a supplier of butt fusion fittings, and over the years, I’ve noticed that many customers struggle with adjusting the pressure during the butt fusion process of fittings. It’s a crucial step, and getting it wrong can lead to all sorts of problems, like leaks or weak joints. So, I thought I’d share some tips on how to adjust the pressure properly. Butt Fusion Fittings
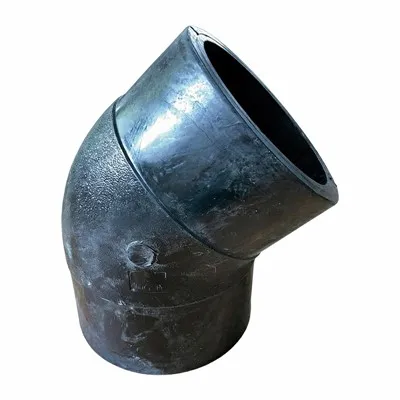
First off, let’s understand why pressure adjustment is so important in the butt fusion process. When you’re fusing two fittings together, the right pressure ensures that the plastic material on the mating surfaces melts and blends uniformly. This creates a strong, leak – free bond. If the pressure is too low, the bond might not be strong enough, and there could be gaps or weak spots. On the other hand, if the pressure is too high, it can cause the plastic to squeeze out too much, leading to a non – uniform joint and potentially weakening the overall structure.
Pre – fusion Preparation
Before you even start thinking about adjusting the pressure, you’ve got to make sure everything is set up correctly. First, clean the surfaces of the fittings that are going to be fused. Any dirt, grease, or debris can affect the quality of the bond. You can use a clean, dry cloth or a special plastic cleaner for this.
Next, measure the outside diameter of the fittings accurately. This is crucial because the pressure required for fusion depends on the size of the fittings. Different sizes need different pressures to achieve the right melt and bond. You can use a caliper to get an accurate measurement.
Determining the Initial Pressure
Once you’ve prepared the fittings, it’s time to set the initial pressure. Most manufacturers provide guidelines on the recommended pressure based on the size and type of fittings. As a general rule of thumb, smaller diameter fittings usually require less pressure compared to larger ones.
For example, for 20mm – 50mm diameter fittings, the initial pressure might be around 0.1 – 0.2 MPa. For larger fittings, say 100mm and above, you might need to start with a pressure of 0.2 – 0.3 MPa. But these are just rough estimates, and you should always refer to the manufacturer’s specifications.
Monitoring the Fusion Process
Now, here comes the tricky part – monitoring the process and adjusting the pressure as needed. When you start the fusion process, the pressure will cause the plastic to soften and start to melt. You’ll notice a bead of molten plastic forming around the joint. This is a good sign that the process is working.
Keep an eye on the size and shape of the bead. If the bead is too small, it might mean that the pressure is too low. In this case, you’ll need to increase the pressure gradually. Just be careful not to increase it too much at once. I usually recommend increasing it by about 0.05 MPa at a time.
On the flip side, if the bead is too large and the plastic is flowing out in an uncontrolled way, the pressure is probably too high. You’ll need to reduce the pressure. Again, do it slowly, about 0.05 MPa at a time.
Temperature Considerations
Temperature also plays a big role in the butt fusion process. The higher the temperature of the heating element, the more easily the plastic will melt. If the temperature is too high, you might need to reduce the pressure slightly because the plastic will be more fluid. Conversely, if the temperature is lower, you might need to increase the pressure a bit to get the right melt.
It’s important to note that different types of plastics have different melting points. For example, polyethylene (PE) has a different melting behavior compared to polypropylene (PP). So, make sure you know the type of plastic your fittings are made of and adjust the pressure and temperature accordingly.
Post – fusion Pressure Adjustment
After the fusion is complete, you still need to maintain some pressure for a short period. This is called the post – fusion pressure. The purpose of this is to allow the joint to cool and solidify under the right conditions. If you release the pressure too soon, the joint might not set properly, and you could end up with a weak bond.
The amount of post – fusion pressure and the duration it needs to be maintained also depend on the size and type of fittings. Generally, for smaller fittings, you might need to maintain a post – fusion pressure of about 0.05 – 0.1 MPa for 1 – 2 minutes. For larger fittings, it could be 0.1 – 0.2 MPa for 3 – 5 minutes.
Troubleshooting Pressure – related Issues
If you’re having problems with the fusion process, here are some common pressure – related issues and how to fix them:
- Weak joints: If the joint seems weak after the fusion, it could be due to low pressure during the fusion process. Check if the pressure was set correctly and if it was maintained throughout the process. You might need to increase the pressure next time.
- Excessive bead formation: As I mentioned earlier, this is a sign of high pressure. Reduce the pressure and make sure you’re not over – applying it during the process.
- Uneven joints: An uneven joint could be a result of inconsistent pressure. Make sure that the pressure is applied evenly across the joint. You might need to check the alignment of the fittings and the pressure – applying equipment.
Conclusion
Adjusting the pressure during the butt fusion process of fittings is a skill that takes some practice. But by following these tips, you can ensure that you get strong, reliable joints every time. Remember to always refer to the manufacturer’s guidelines, monitor the process closely, and make adjustments as needed.
PPR Fittings If you’re in the market for high – quality butt fusion fittings and need more advice on the fusion process, I’m here to help. Reach out to me and we can discuss your specific needs. Whether you’re a small DIY enthusiast or a big – time construction company, we’ve got the right fittings for you. Let’s work together to make your projects a success!
References
- Plastic Pipe and Fitting Handbook
- Manufacturer’s manuals for butt fusion fittings
Qingdao Polyfusion Machinery Co., Ltd.
As one of the most professional butt fusion fittings manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy bulk high quality butt fusion fittings from our factory.
Address: Chengyang Industry Zone, Chengyang, Qingdao, Shandong, China
E-mail: export01@qdpolyfusion.com
WebSite: https://www.polyfusionfittings.com/
